
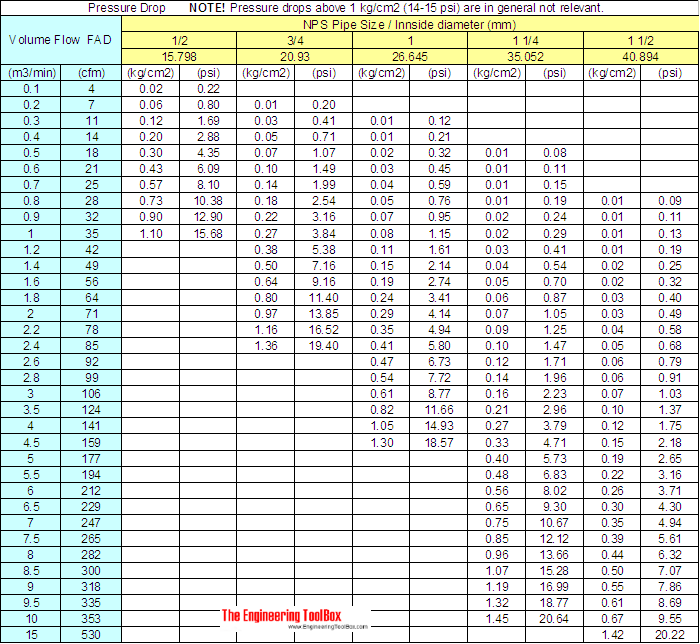
Industrial Burner Velocity and Friction: Is 3 psi/100 ft Pressure Drop Gradient on Gas Lines Okay on Long-Run High-Pressure Headers?
Ever walked down a pipe rack in a mid-sized chemical plant, looked up at a massive four-inch natural gas header, and wondered if the fluid dynamics engineer who sized it was having a good day? You aren't alone. We have all been there, standing next to a roaring multi-megawatt combustion system, staring at a pressure gauge that seems just a little too eager to drop off a cliff. Piping design for high-demand industrial burners is one of those classic engineering fields where rule-of-thumb traditions frequently collide head-on with physics.
So, let us address the elephant in the room right away. Is a 3 psi per 100 feet pressure drop gradient acceptable on long-run high-pressure natural gas lines feeding industrial burners? The short answer? It depends, but usually, it is playing with fire—and not the good kind your burner is supposed to make. If you are pushing high volumes over hundreds of feet, relying on that aggressive drop gradient can lead to severe system instability, starving equipment, and localized high velocities that chew up your pipe walls.
Designing a rock-solid fuel train requires balancing raw flow capacity against friction losses without turning your piping network into a giant bottleneck. When you run high-pressure headers across a sprawling facility, every single psi matters. Let us strip away the overly dense textbook equations for a moment and look at what is actually happening inside that high-pressure steel pipe when your combustion system calls for maximum firing rate.
Honestly, sizing gas lines for industrial burners should never be a guessing game. Yet, plant retrofits routinely force higher flow rates through legacy piping networks original designers never intended for such loads. The result? Excessive pressure drops, unexpected control valve hunting, and flame safety systems tripping out at the absolute worst times.
Understanding Gas Dynamics and Friction in Industrial Fuel Lines
Let us talk about fluid dynamics without getting bogged down in overly formal academic nonsense. When natural gas flows through a pipe, it experiences resistance against the internal pipe wall. This continuous interaction creates friction, which directly converts useful static pressure into friction loss and thermal energy. The rate at which this pressure dissipates over distance is what engineers refer to as the pressure drop gradient, commonly measured in psi per 100 feet of straight pipe.
Gas is compressible, which makes this dynamic entirely different from liquid piping design. As the static pressure drops along the length of a long header, the gas expands. When the gas expands, its volumetric flow rate increases, which forces the flow velocity to ramp up even further. It is a compounding problem. What started as a reasonable line speed at the supply skid can quickly accelerate into an aggressive, turbulent roar near the end of a long run.
Calculating the true loss in long-run gas lines involves evaluating the interaction between boundary layer friction, line density, and overall Reynolds numbers. High friction causes local turbulence, which distorts the velocity profile inside the pipe. When this distorted flow reaches your fuel control valves or flow meters, it ruins measurement accuracy and makes precise air-fuel ratio tuning almost impossible.
Look, high pressure changes the calculus slightly because high-density gas experiences different shear stresses along the pipe wall compared to low-pressure fuel systems. However, pushing a standard industrial burner velocity and friction design past reasonable limits usually ends in operational headaches. You cannot simply boost the regulator pressure upstream and pretend the line friction magically disappears.
The Real Physics Behind Friction Factor and Line Velocity
Friction loss isn't linear when compressibility enters the picture. As natural gas line friction loss accumulates over a 500-foot header, the downstream density drops, forcing the actual gas velocity to rise significantly to maintain the same mass flow rate. If your baseline velocity starts at 60 feet per second, that cumulative expansion might push line speed past 100 feet per second before the gas even reaches the final burner take-off branch.
High velocity generates localized noise, physical pipe vibration, and extreme mechanical stress on inline components like strainers, check valves, and regulators. The Darcy-Weisbach and Weymouth equations remind us that friction scales aggressively with line speed. Double your gas velocity, and you quaduply your dynamic friction losses. That is a brutal trade-off when attempting to run a tight pressure drop tolerance across long distances.
Furthermore, internal pipe roughness plays a massive role in actual performance. Schedule 40 carbon steel piping might feature smooth walls when brand new, but years of subtle moisture exposure, scale buildup, and field welds turn that smooth internal profile into a rough track. That added roughness rapidly increases the Moody friction factor, turning what was once a calculated 2 psi drop into a real-world 4 psi loss.
Compressibility Factor and High-Pressure Effects
At high operating pressures—say, 30 to 60 psig or higher—natural gas deviates notably from ideal gas behavior. The compressibility factor ($Z$) dictates how dense the medium remains under static pressure. Sizing headers based on simple low-pressure standard cubic feet per hour (SCFH) rules routinely leads to miscalculated pipe schedules and inadequate fuel volume delivering to the burner train.
When high-pressure gas moves down a restrictive header with a 3 psi/100 ft drop, the sudden pressure differential across long runs alters the gas density dramatically. This variable density creates shifting pressure conditions at each burner takeoff line along the header. The first burner along the rack gets rich, high-density fuel at nominal pressure, while the final burner down the line gets starved, lower-density fuel, leading to uneven firing rates.
Evaluating gas piping pressure drop per 100 feet requires accounting for real-world compressibility shifts. Ignoring these shifts means your front-end burners will run completely fine while your back-end burners struggle with unstable flames, high carbon monoxide emissions, or nuisance flame-outs during peak plant capacity cycles.
Evaluating the 3 psi/100 ft Gradient Rule on Long-Run Headers
Is a 3 psi per 100 feet pressure drop gradient okay for a long-run high-pressure gas header? In short: for short distribution runs, it is often manageable, but for long-run headers, it is usually a recipe for systemic operational failure. If your main header extends 300, 500, or 800 feet across a plant footprint, taking a 3 psi loss every single 100 feet consumes massive amounts of total system pressure reserve before the fuel even hits the burner gas train.
Consider the math for a second. On a 500-foot header run, a 3 psi/100 ft gradient equates to a cumulative pressure loss of 15 psi across the main distribution line alone. If your incoming supply regulator is set to 30 psig, your available pressure at the end of the line has dropped by 50 percent down to 15 psig. That massive drop forces down-stream control valves to open wider, destroying your control turndown ratio and severely limiting maximum thermal output.
Most veteran combustion engineers target a much more conservative pressure drop gradient for long main headers—typically between 0.5 psi and 1.5 psi per 100 feet. This keeps overall gas velocities at reasonable levels, prevents unwanted pressure drops across the facility, and guarantees that every burner branch receives stable, predictable inlet pressure regardless of plant firing demand.
Designing around a tight line sizing standard gives your system critical breathing room for future facility expansions. If you design your main gas header right up against the 3 psi limit today, you will have zero spare capacity when management decides to install another boiler or process heater on that same line next year.
High Velocity Risks in Fuel Gas Systems
Running high pressure drops inevitably means running high gas velocities inside the pipe. When line speeds push past 100 to 120 feet per second in fuel gas lines, bad things start to happen. The sheer mechanical energy of high-velocity gas creates loud, low-frequency acoustic noise that echoes through support structures and violates workplace safety noise limits.
Worse yet, extremely high gas velocity induces mechanical vibration that fatigues threaded joints, instrument taps, and control valve trim over time. High velocity also picks up fine rust, pipe scale, or mill debris inside the header, blasting downstream regulator seats and valve seals like a low-grade sandblaster. Keeping velocities under control is essential for long-term mechanical reliability.
A tight line design balances internal gas speed with acceptable friction limits. Staying well clear of acoustic velocity thresholds protects your sensitive instrumentation, extends control valve life, and maintains steady, whisper-quiet fuel delivery straight to the combustion zone.
Burner Turndown Ratio and Control Valve Instability
Burner systems rely on precise, repeatable gas pressures to maintain safe air-fuel ratios across their entire operating turndown range. If your main header suffers from an aggressive high pressure gas header design loss, the pressure feeding the gas train varies wildly depending on how many other burners in the plant are firing simultaneously.
Imagine setting up a burner train when the rest of the plant is idling. You tune your air-fuel ratios perfectly. Then, two hours later, three massive process heaters online elsewhere on the network start pulling maximum fuel demand. The header pressure at your burner drops 10 psi due to the severe line gradient, instantly starving your flame and causing the air-fuel ratio to drift dangerously lean.
This dynamic cross-talk between burners degrades control stability, causes control valves to hunt violently, and can easily trigger low-gas-pressure limit switches. Safe, reliable operation demands a rock-solid, stable supply header where local line losses stay minor regardless of overall plant demand swings.
Best Practices for Sizing High-Pressure Industrial Gas Lines
Sizing gas headers for industrial plants requires looking beyond basic sizing charts found in standard plumbing codes. Industrial high-pressure headers handling thousands of standard cubic feet per minute require explicit engineering calculations that account for velocity limits, pipe schedules, total equivalent length of fittings, and future load expansion.
Always size your main distribution headers based on continuous velocity constraints rather than arbitrary pressure drop limits alone. A practical rule of thumb for long-run high-pressure natural gas headers is to limit gas velocity to 60–80 feet per second under maximum peak load while targeting a pressure drop gradient between 0.5 and 1.0 psi per 100 feet.
Additionally, take time to carefully calculate the equivalent length of all inline valves, elbows, tees, and strainers. A single 90-degree sharp elbow or restrictive isolation valve can easily add 30 to 50 equivalent feet of straight pipe friction to your header calculation. Ignoring these inline fittings leads to unexpected real-world pressure drops that exceed your paper designs.
Finally, always design headers using a top-down approach that prioritizes pressure regulator droop allowances, control valve authority, and minimum burner manifold requirements. Let us outline a practical step-by-step sizing framework for heavy industrial installations.
Engineering Design Steps for High-Pressure Lines
- Establish Peak Thermal Load: Calculate the total combined maximum firing rate of all connected burners, including a 15–20% safety margin for future expansion, and convert this value into peak actual cubic feet per hour (ACFH) at operating pressure.
- Determine Supply and Terminal Pressure Limits: Identify the minimum guaranteed supply pressure at the main regulator and establish the absolute minimum inlet pressure required at the furthest burner's double block and bleed valve train.
- Select Target Velocity Limits: Limit maximum gas velocity to 60–80 ft/s inside long distribution headers, reserve higher speeds (up to 100 ft/s max) strictly for short, localized branch drop lines directly at the burner.
- Calculate Equivalent Length: Measure the total physical distance of the pipe run and add the equivalent straight-pipe length for every elbow, tee, reducer, manual valve, and inline instrument tap.
- Compute Pressure Gradient: Calculate the calculated pressure drop gradient using compressible flow formulas like Weymouth, Panhandle B, or Darcy-Weisbach, verifying the gradient stays between 0.5 and 1.5 psi/100 ft.
- Verify Control Valve Authority: Ensure downstream control valves maintain at least 30–50% of the total system pressure drop to preserve proper control authority across the entire turndown range.
Comparison: Pipe Sizing Strategies for Industrial Gas Headers
To help visualize how different design parameters affect line performance, review this side-by-side comparison of standard sizing approaches for high-pressure industrial fuel headers:
- Aggressive Sizing (3.0+ psi/100 ft Gradient): Small pipe footprint, low initial capital pipe cost, but results in high line velocities (>100 ft/s), extreme pressure drop over long runs, valve hunting, noise, pipe vibration, and zero capacity for plant expansion.
- Standard Industrial Sizing (1.0 - 1.5 psi/100 ft Gradient): Moderate pipe diameter, balanced material costs, stable line velocities (60–80 ft/s), low noise, predictable control valve performance, and minor baseline allowance for added demand.
- Conservative Sizing (<0.5 psi/100 ft Gradient): Larger pipe diameter, higher up-front material cost, extremely low line velocities (<40 ft/s), virtually zero pressure drop over long distances, superior system stability, and massive capacity for future plant growth.
Common Questions About Industrial Gas Line Velocity and Friction
Is a 3 psi/100 ft pressure drop ever acceptable on gas lines?
Yes, but typically only on very short, localized branch drops right at the equipment train where the overall distance is less than 20 to 30 feet. On long main headers extending hundreds of feet, maintaining a 3 psi/100 ft gradient causes massive cumulative pressure loss, high line velocities, and systemic flame instability.
What is the recommended maximum gas velocity for industrial fuel headers?
For long distribution headers, ideal gas velocities should be kept between 60 and 80 feet per second. Short branch lines feeding individual burners can occasionally run up to 100 feet per second, but exceeding 120 feet per second risks severe pipe vibration, acoustic noise violations, and erosion of internal valve components.
How does natural gas line friction loss affect burner control systems?
Excessive line friction loss causes significant pressure fluctuations at the burner supply train whenever overall plant demand changes. This pressure instability ruins control valve authority, causes air-fuel ratios to shift lean or rich, distorts flow meter readings, and can cause unexpected low-gas-pressure trips during peak operations.
Which equation should I use for high-pressure gas line calculations?
The Weymouth equation is widely used for high-pressure industrial gas distribution lines operating above 30 psig, as it accounts for high volume throughput and internal friction. The Darcy-Weisbach equation combined with real gas density evaluations is also excellent for high-accuracy engineering calculations over long header runs.